Mechanical Seals for Pumps
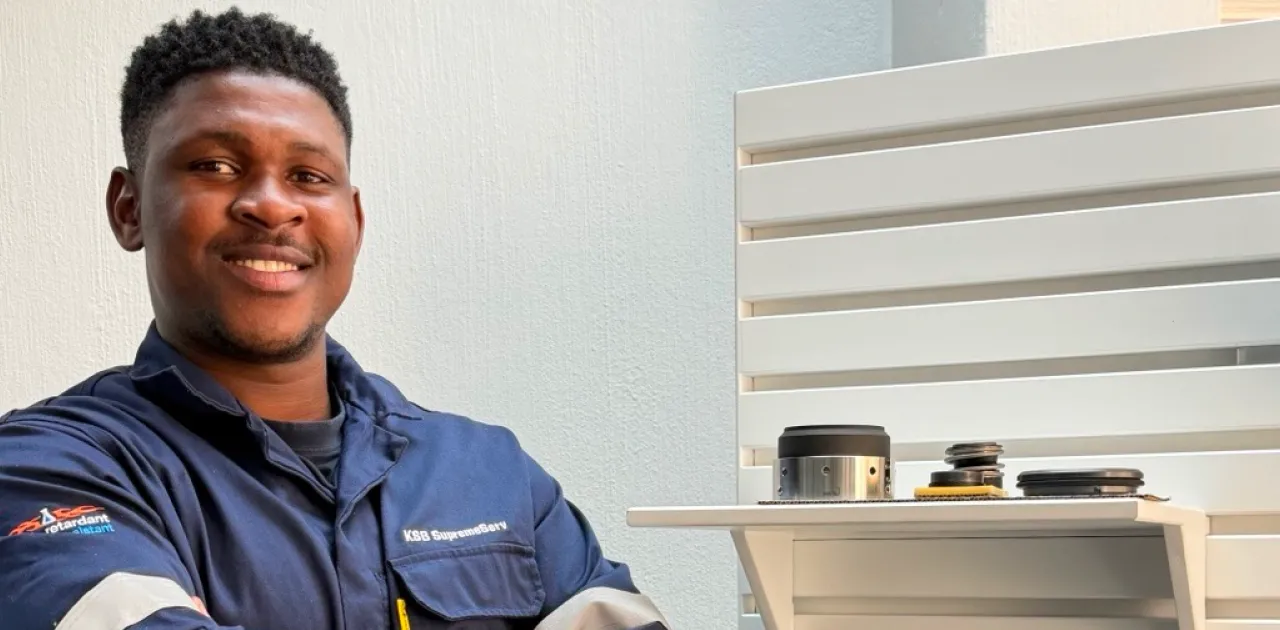
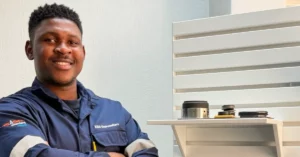
“Most people know KSB Pumps and Valves as a pump manufacturer and are surprised to learn that we also design, manufacture and support our own range of mechanical seals for nearly every pump type and that we are continually introducing solutions for competitor products too,” says KSB SupremeServ sales engineer for mechanical seals, Phumelela Ngcobo,
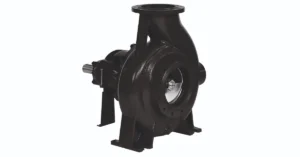
The company is already producing a large portion of the seals used in its new pumps and has recently begun marketing and raising awareness of its sealing solutions. “The roles of mechanical seals are important for the reliable operation of many types of pumps as their primary purpose is to prevent the pumped material from leaking along the rotating shaft in order to ensure that the fluid remains safely contained within the pump and doesn’t leak into the surrounding environment.”
Detailed understanding
Phumelela explains that it was during the development of one of KSB’s pump ranges that company engineers encountered recurring seal failures that could not simply be resolved by changing operating practices.
“Because we know and understand pump designs we have a detailed understanding of hydraulic performance, shaft behaviour, bearing arrangements and the operating conditions inside the seal chamber. This allowed our engineers to identify the root causes of the failures and develop sealing solutions specifically designed to overcome those challenges.
Vast majority
“Today our range includes sealing solutions for the vast majority of KSB pumps together with universal mechanical seals suitable for many competitor brands. Where a standard solution is unavailable, our engineering team will even develop custom sealing systems based on pump dimensions and detailed process information supplied by the customer,” Phumelela adds.
The range includes component and cartridge mechanical seals available in both single and dual arrangements. It also comprises pump-specific sealing solutions, seals manufactured in accordance with DIN EN 12756, API 682-compliant sealing systems for applicable process pumps, slurry application seals, boiler feed pump seals, high-pressure mechanical seals, and ATEX-certified sealing solutions for use in hazardous environments.
Integrated package
A considerable advantage of manufacturing mechanical seals is the ability to offer customers complete sealing solutions from a single source. In addition to mechanical seals, the portfolio includes API 682-compliant seal support systems, piping plans, seal pots, heat exchangers, flow meters, and associated instrumentation.
Supplying these components as an integrated package ensures compatibility between the sealing equipment and support system simplifying procurement, installation, commissioning and ongoing maintenance while enhancing overall system reliability.
Reliable performance
It is important to note that every application is unique and the materials selected for a mechanical seal are chosen to maximise reliability under the specific operating conditions. For general industrial duties, Reaction Bonded Silicon Carbide (RBSiC) is often the preferred choice offering excellent wear resistance and reliable performance across a wide range of applications.
For more demanding services involving aggressive chemicals, elevated temperatures or higher operating pressures Sintered Silicon Carbide (SSiC) is typically specified due to its corrosion resistance, higher mechanical strength and excellent performance under severe operating conditions.
Demanding conditions
“Carbon is widely used as a seal face material due to its excellent self-lubricating properties and low coefficient of friction making it ideal for clean fluid applications across a range of industries including food and beverage processing.
“For more demanding operating conditions involving higher temperatures and pressures, antimony-impregnated carbon is often specified because of its improved mechanical strength, wear resistance and enhanced thermal conductivity,” Phumelela explains.


Making a choice
“Where pumps handle abrasive slurries or fluids containing suspended solids, tungsten carbide is frequently selected for its exceptional hardness and outstanding resistance to abrasive wear that ensures reliable performance in severe service conditions.
“Standard metallic components are manufactured from 316L stainless steel, while highly corrosive applications may require upgraded materials such as Super Duplex Stainless Steel. Secondary sealing elements are also carefully selected with elastomers including FKM (Viton), EPDM and FFKM (Perfluoro elastomer/Kalrez) specified according to the chemical compatibility and operating temperature of each application.
Discourage guesswork
“There are many variables so it pays to deal with our team rather than guess. Every seal is engineered using the most appropriate combination of materials for the customer’s operating conditions,” says Phumelela.
KSB mechanical seals are used across a wide spectrum of industries including mining, water and wastewater, petrochemical processing, power generation, pulp and paper production, chemical processing, food and beverage manufacturing and general industry among others.
Passing the test
These are supported by KSB SupremeServ’s dedicated refurbishment facilities which repairs KSB and competitor mechanical seals.
“Every seal that enters our workshop undergoes a detailed inspection before refurbishment. Once assembly has been completed, it is pressure tested to ensure it meets our quality standards. No refurbished seal leaves our workshop without successfully passing the test.”
The Full Monty
KSB’s aftermarket support extends well beyond workshop repairs. Field service technicians provide mechanical seal installation, auxiliary system installation, commissioning assistance, seal failure investigations and on-site technical support to assist customers in identifying the underlying causes of premature failures rather than simply replacing damaged components.
KSB SupremeServ also offers complimentary technical training covering mechanical seal fundamentals, seal selection, API 682 piping plans, auxiliary systems, installation best practices and seal failure analysis. In addition, continuous product training is provided to KSB sales engineers and authorised sales partners to ensure customers receive technically sound advice from knowledgeable sealing specialists.